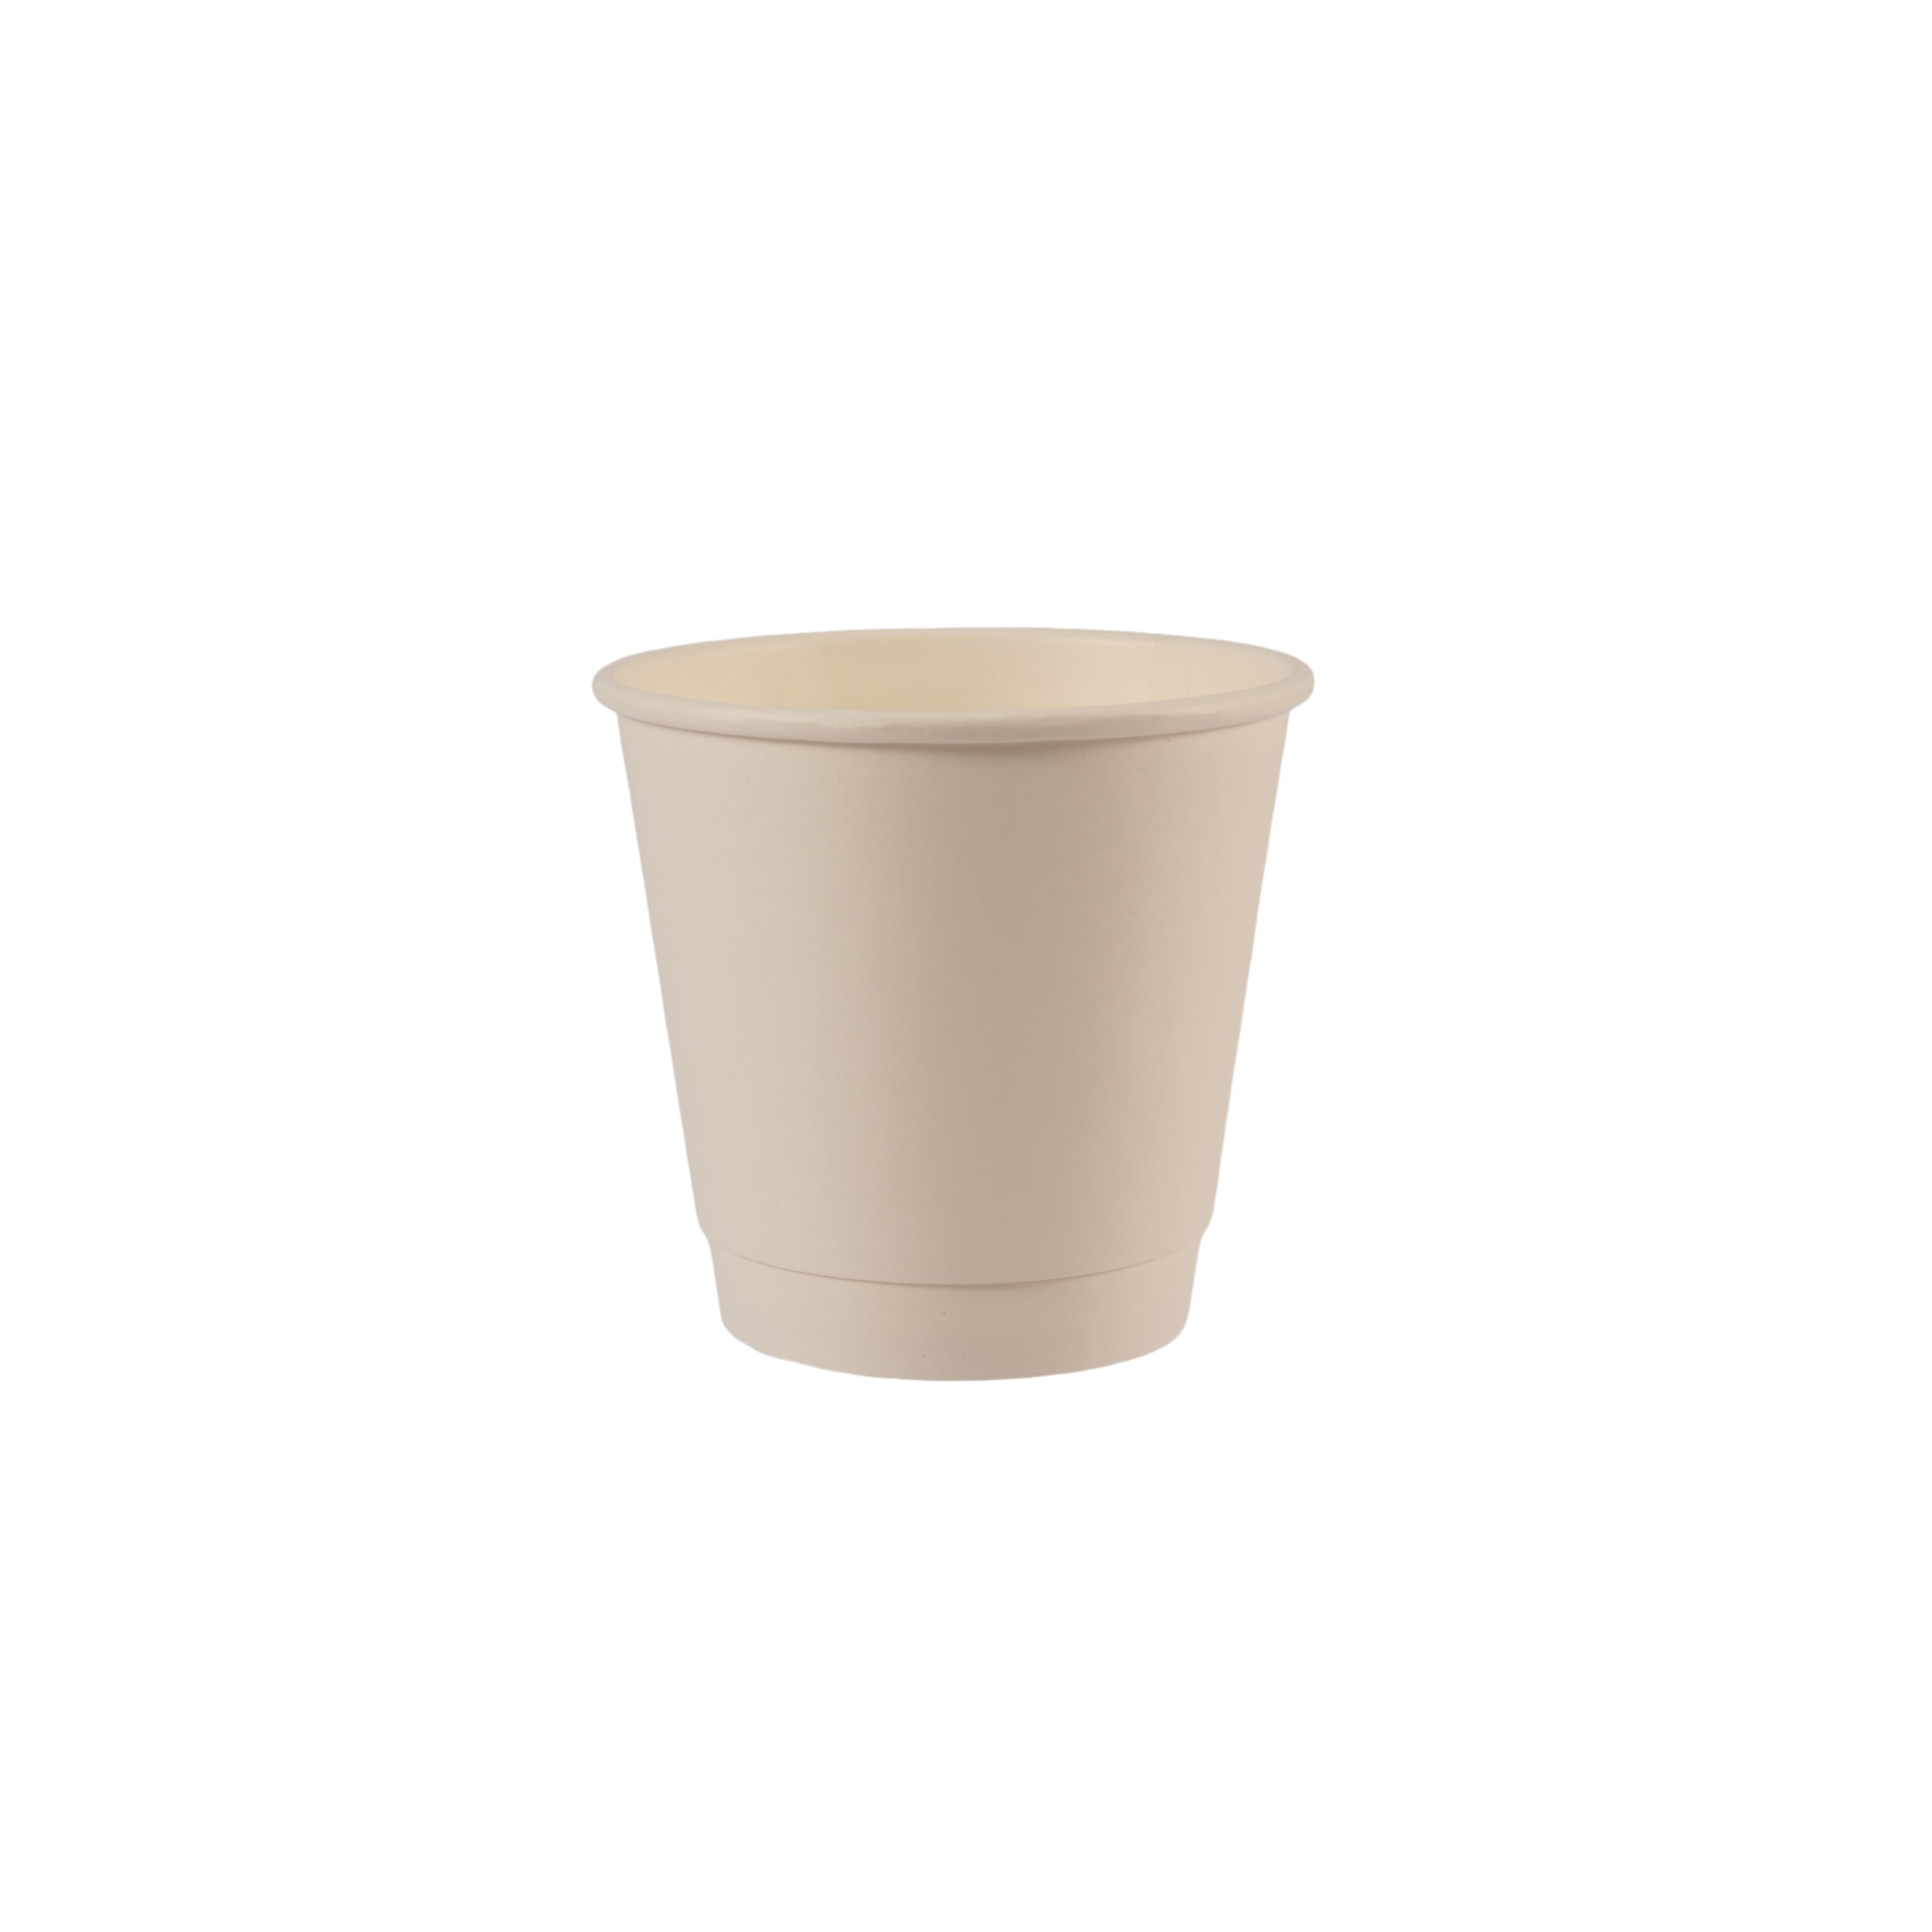
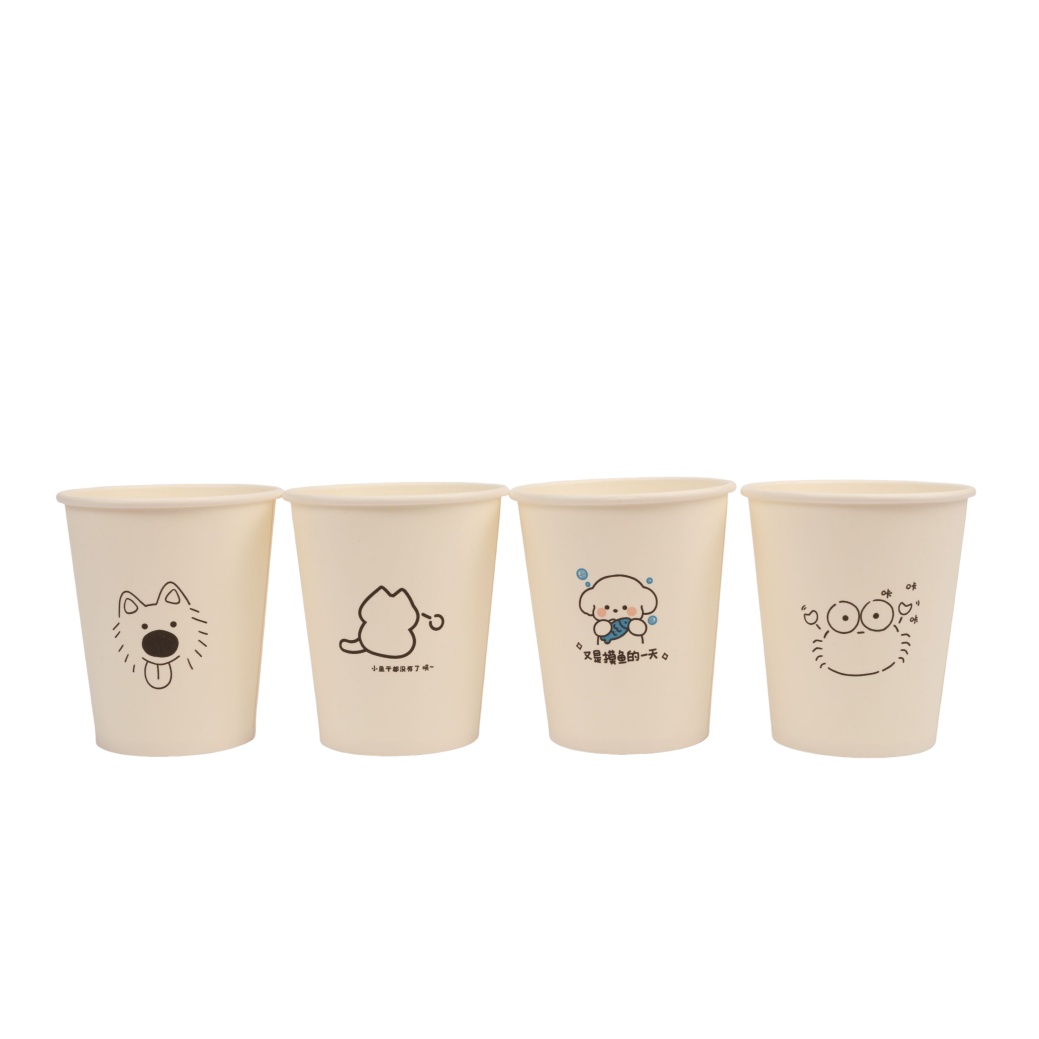
100ml Paper Cup | Premium Beverage Cups

, , 
Inquiry
Inquiry

100ml paper cup

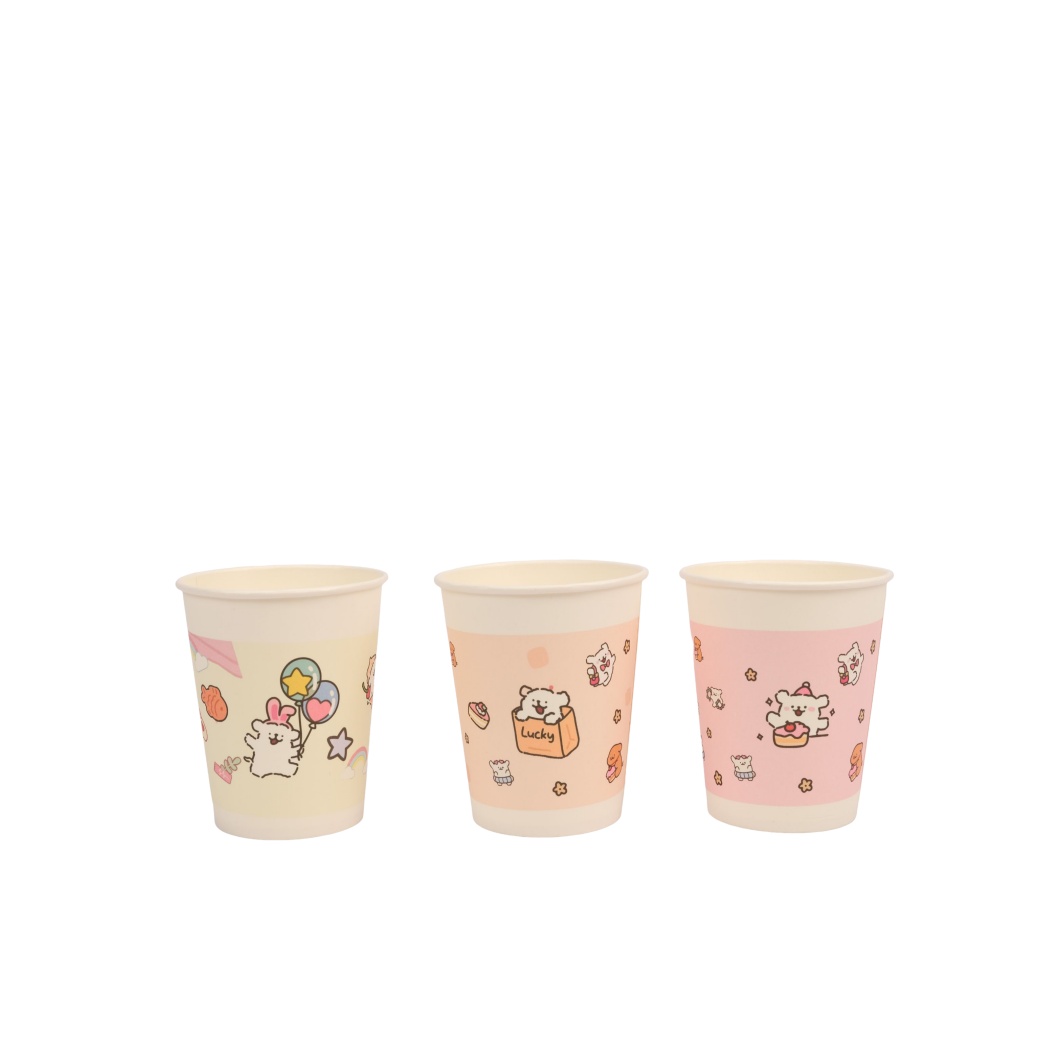
The 100ml paper cup represents an essential beverage container solution designed for cafes, restaurants, offices, and events. This compact 100ml paper cup serves multiple purposes, making it ideal for espresso shots, samples, and portion control applications. The 100ml paper cup combines functionality with sustainability, offering businesses a practical choice for serving hot and cold beverages. Technologically, the 100ml paper cup features advanced manufacturing that ensures durability and liquid resistance. The paper construction includes a food-grade polyethylene coating that prevents leakage while maintaining environmental responsibility. This coating system allows the 100ml paper cup to withstand temperatures up to 90 degrees Celsius, making it suitable for various hot beverage applications. The 100ml paper cup incorporates precision engineering with reinforced walls that provide structural integrity during transport and handling. The rim design prevents splashing, while the base offers stability on any surface. Print quality on the 100ml paper cup remains vibrant, allowing businesses to showcase branding effectively. Applications for the 100ml paper cup extend across multiple industries. Coffee shops utilize this size for espresso and specialty shots, while healthcare facilities use it for medication cups. The 100ml paper cup also serves restaurants for sauce dispensing and catering companies for sample portions. Event organizers appreciate the 100ml paper cup for tastings and promotional activities. Educational institutions implement the 100ml paper cup in laboratory settings. This versatile container addresses diverse needs while maintaining consistent quality and performance standards.
The 100ml paper cup delivers exceptional value through its cost-effectiveness and operational efficiency. Businesses purchasing the 100ml paper cup benefit from reduced material costs compared to larger containers while maintaining premium quality standards. The compact size of the 100ml paper cup maximizes storage efficiency, allowing businesses to stock substantial quantities within limited space constraints. Operational advantages of the 100ml paper cup include simplified inventory management and faster serving times. Staff efficiency improves when using the 100ml paper cup since the standardized size eliminates measurement uncertainty and accelerates service delivery. The 100ml paper cup reduces waste through precise portioning, directly impacting profit margins and environmental sustainability efforts. Customers appreciate the 100ml paper cup for its convenient size and practical applications. The 100ml paper cup prevents over-purchasing when customers want to sample products before committing to larger quantities. This container size encourages trial purchases across food and beverage sectors, particularly benefiting specialty coffee shops and gourmet establishments. The 100ml paper cup supports business sustainability goals through its recyclable paper composition. Companies implementing the 100ml paper cup demonstrate environmental commitment while maintaining operational excellence. The 100ml paper cup's lightweight design reduces shipping costs and carbon footprint throughout the supply chain. Marketing advantages emerge when utilizing the 100ml paper cup, as branded messaging appears prominently on the container surface. Customers interact with branding throughout their purchase experience, increasing brand recall significantly. The 100ml paper cup serves as a portable advertisement, extending marketing reach beyond the point of sale and generating organic brand visibility in public spaces.

Practical Tips

Industry News: PE/PLA Coated Paper Leads New Environmental Trend in Food Packaging

29

May

Industry News: PE/PLA Coated Paper Leads New Environmental Trend in Food Packaging

View More
Industry News: Customized Eco-friendly Paper Cups Lead New Trends in Catering and Events

29

May

Industry News: Customized Eco-friendly Paper Cups Lead New Trends in Catering and Events

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Optimal Size for Portion Control and Sampling

Optimal Size for Portion Control and Sampling

The 100ml paper cup provides the perfect volume for precise portion management across hospitality and retail environments. This size enables businesses to serve accurate measurements without wastage, critical for coffee shops offering espresso and specialty beverages. The 100ml paper cup proves invaluable for restaurants conducting sauce and condiment service with consistent portioning. Retailers benefit from the 100ml paper cup when offering product samples, encouraging customer trials and purchase conversions. The 100ml paper cup's capacity works perfectly for medical facilities requiring standardized medication containers. Educational institutions utilize the 100ml paper cup in laboratory environments for chemical measurement and experimentation. Event organizers leverage the 100ml paper cup for tastings and promotional activities at exhibitions and conferences. The 100ml paper cup maintains quality integrity while delivering practical functionality across diverse applications. This specialized size eliminates guesswork in serving procedures, streamlining operations and enhancing customer satisfaction.
Food-Grade Safety and Temperature Resistance

Food-Grade Safety and Temperature Resistance

The 100ml paper cup meets rigorous food safety standards with its premium food-grade polyethylene coating that prevents harmful chemical leaching. This advanced barrier technology in the 100ml paper cup protects beverage quality while maintaining regulatory compliance across all markets. The 100ml paper cup withstands temperatures up to 90 degrees Celsius, accommodating hot espresso, tea, and specialty coffee preparations without compromise. The reinforced construction of the 100ml paper cup prevents deformation under thermal stress, ensuring professional presentation consistently. The 100ml paper cup's moisture-resistant properties eliminate seepage and maintain structural integrity throughout usage periods. Businesses choosing the 100ml paper cup gain peace of mind knowing customers receive beverages in safe, reliable containers meeting international food service standards. The 100ml paper cup's design prevents condensation issues while maintaining the aesthetic appeal of branded surfaces. This reliable performance makes the 100ml paper cup the trusted choice for quality-conscious businesses.
Eco-Friendly Solution with Recyclable Materials

Eco-Friendly Solution with Recyclable Materials

The 100ml paper cup represents sustainable packaging innovation through its recyclable composition and minimal environmental footprint. Businesses implementing the 100ml paper cup demonstrate genuine commitment to ecological responsibility while maintaining operational excellence. The 100ml paper cup's paper-based construction biodegrades naturally, unlike plastic alternatives, reducing landfill contribution significantly. The lightweight design of the 100ml paper cup decreases shipping weight and transportation emissions throughout supply chains. Companies adopting the 100ml paper cup align with corporate sustainability initiatives and meet evolving consumer environmental expectations. The 100ml paper cup's manufacturing process utilizes responsible forestry practices, supporting renewable resource management. Customers increasingly prefer the 100ml paper cup, recognizing environmental consciousness in business practices. The 100ml paper cup enables businesses to reduce plastic dependency while serving quality beverages. This eco-friendly choice positions the 100ml paper cup as the preferred container for environmentally aware organizations seeking sustainable alternatives without sacrificing performance.