Paper Cup Raw Material Manufacturer

, , 
Inquiry
Inquiry

paper cup raw material manufacturer

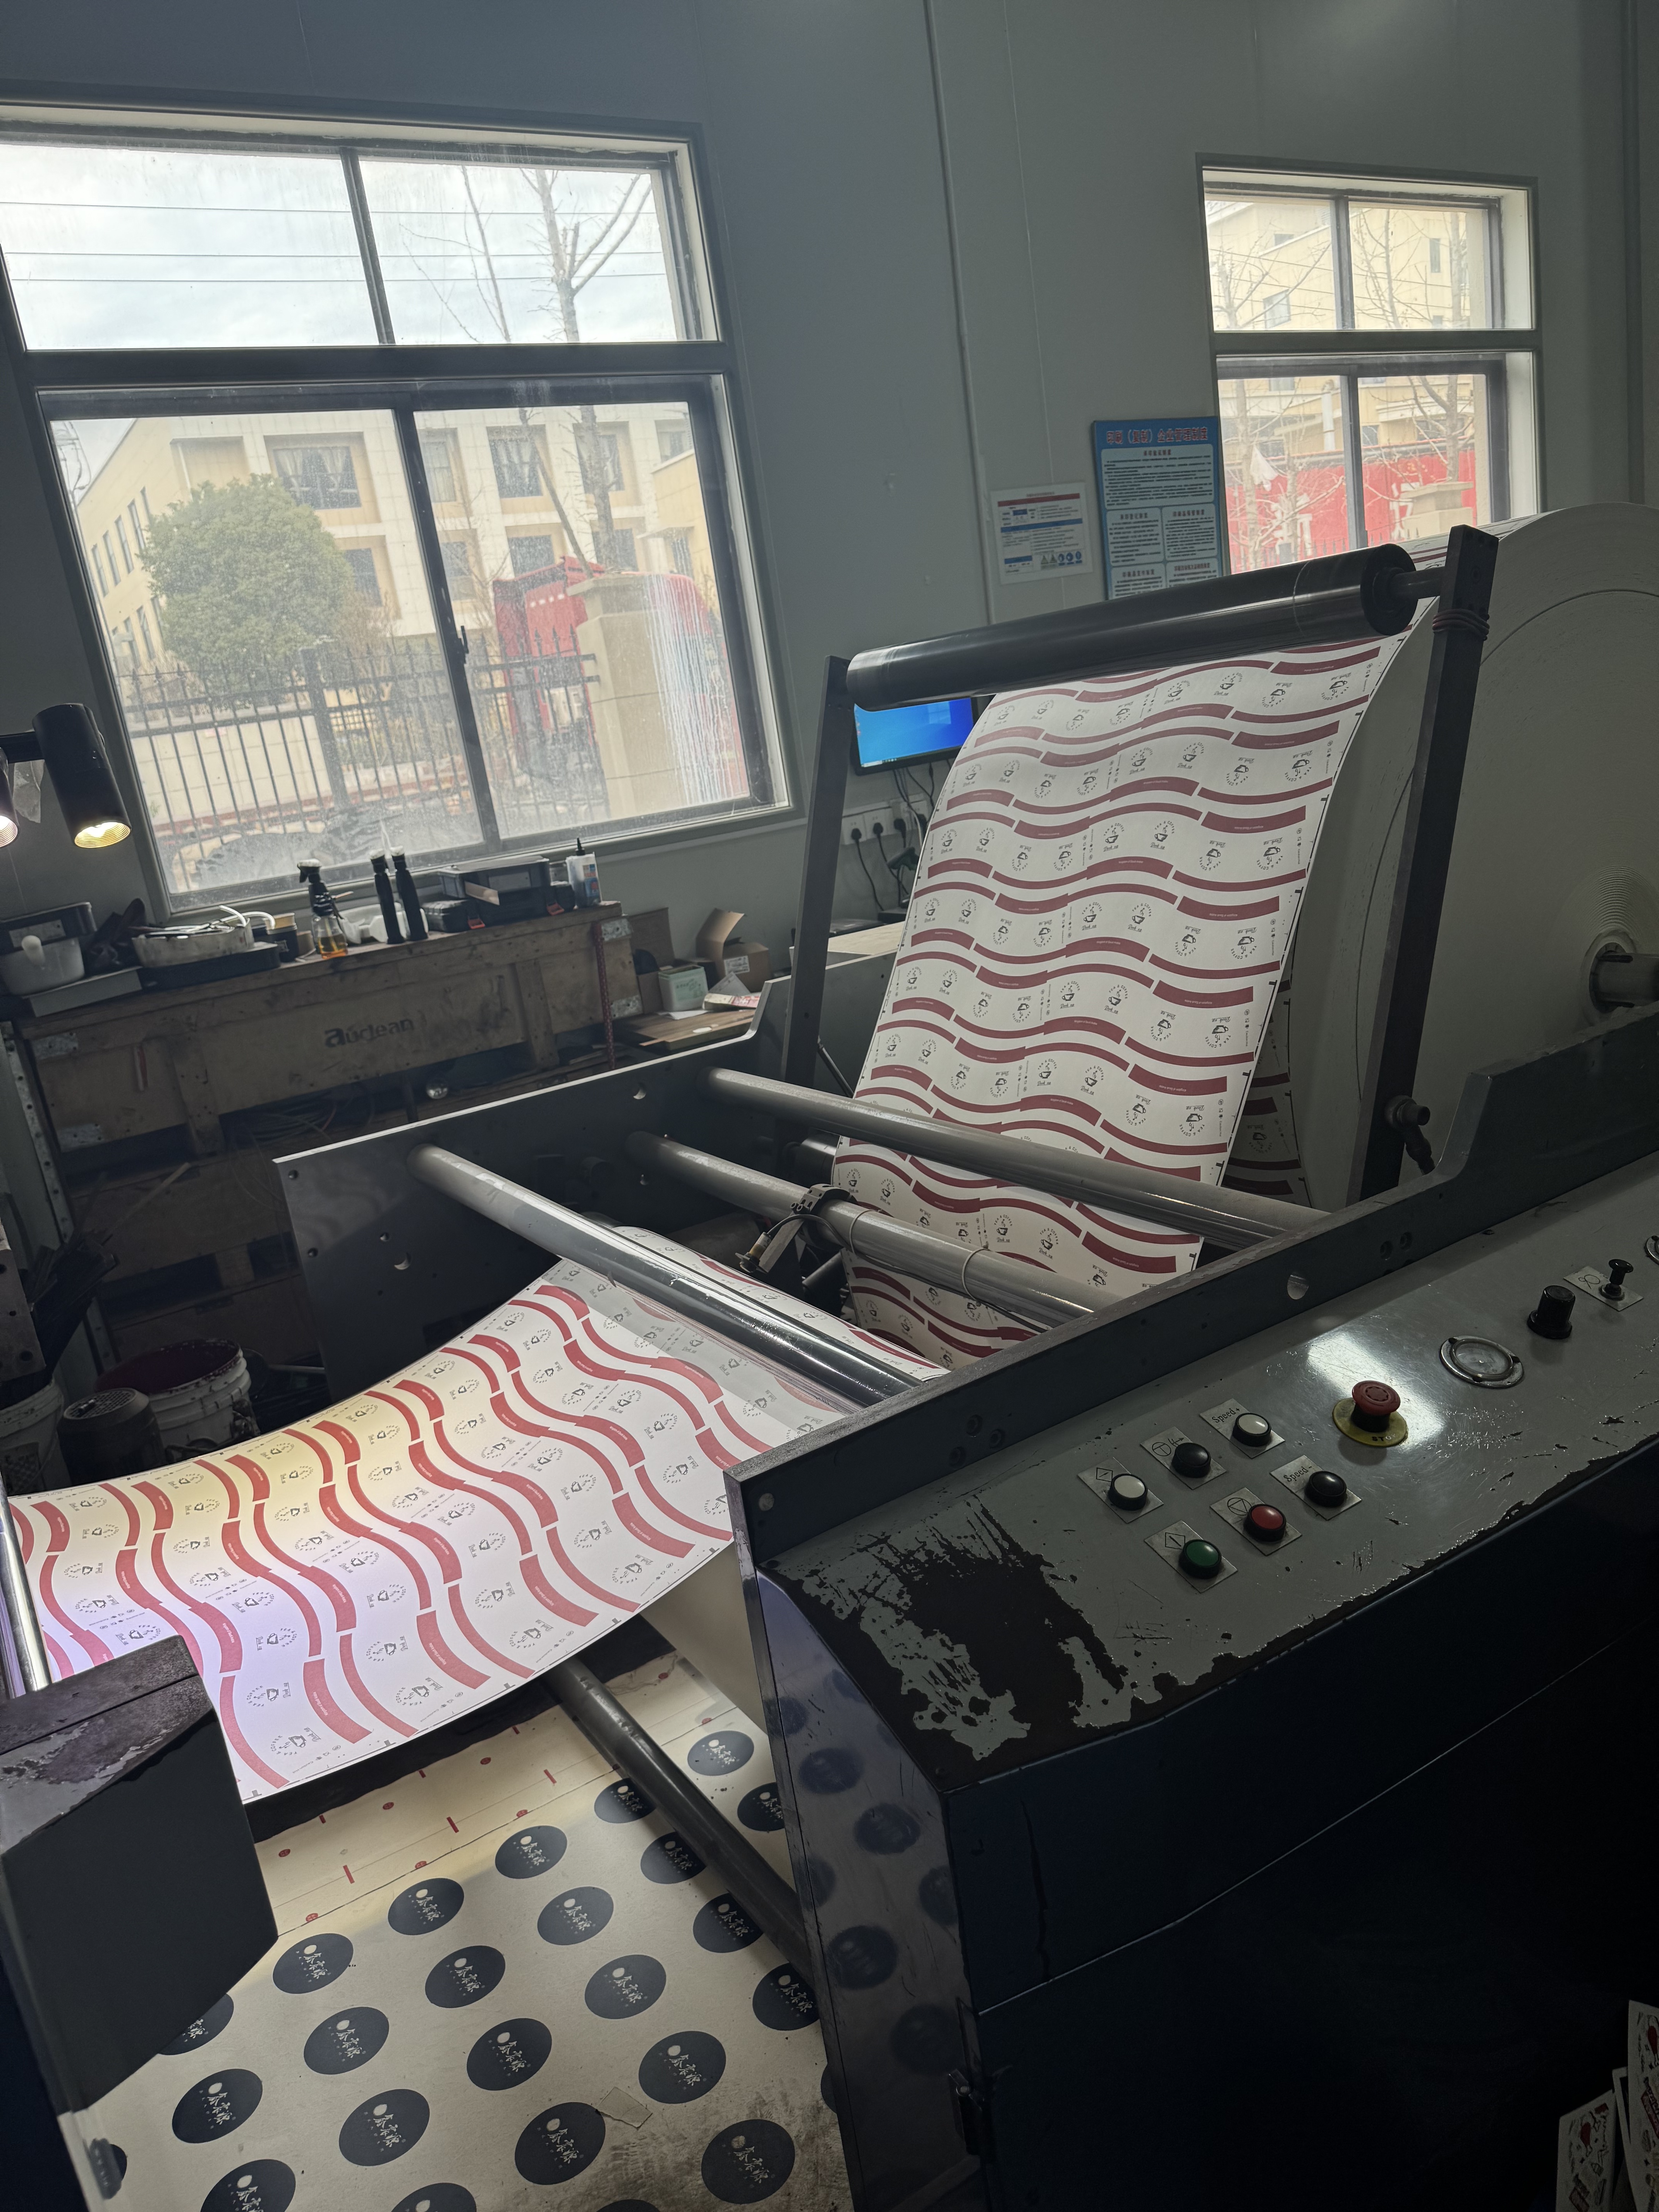
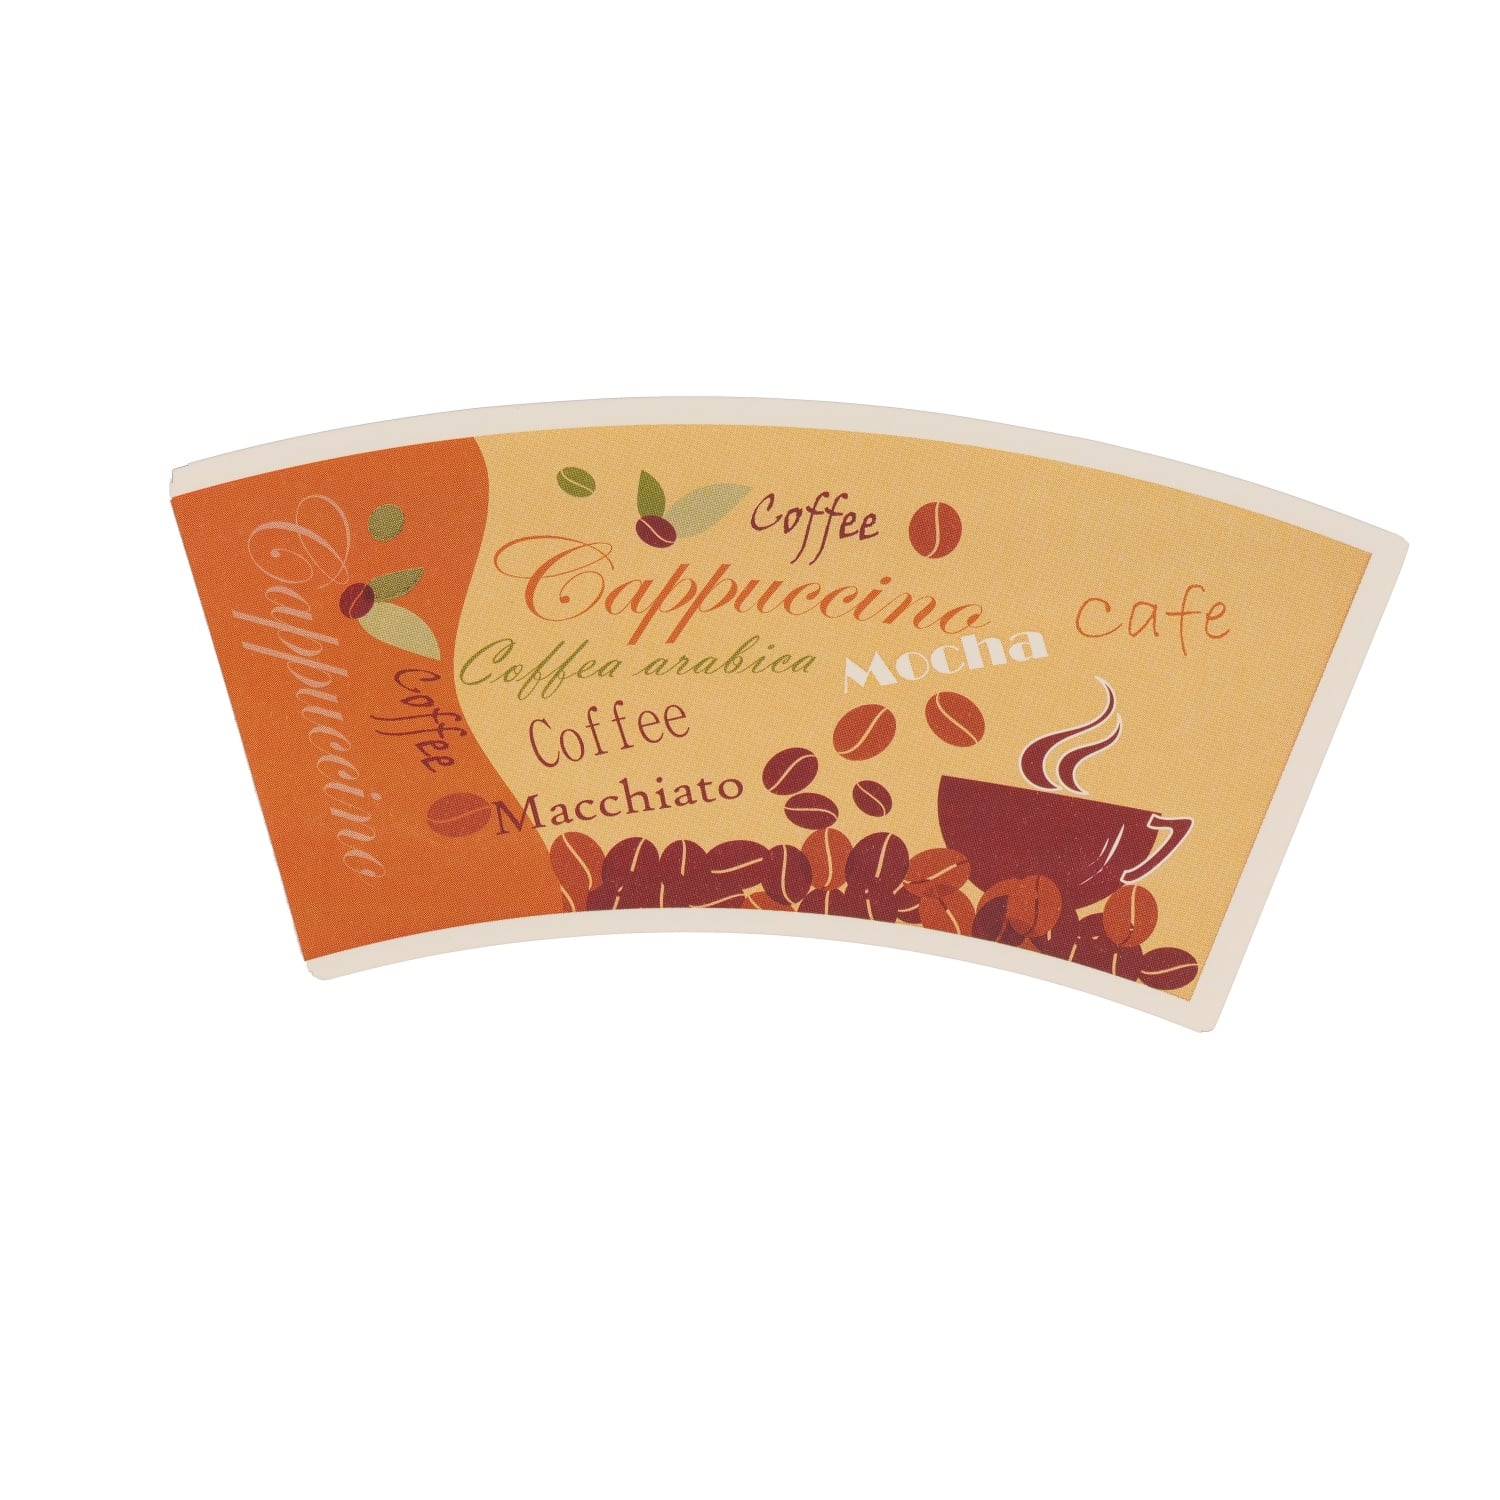
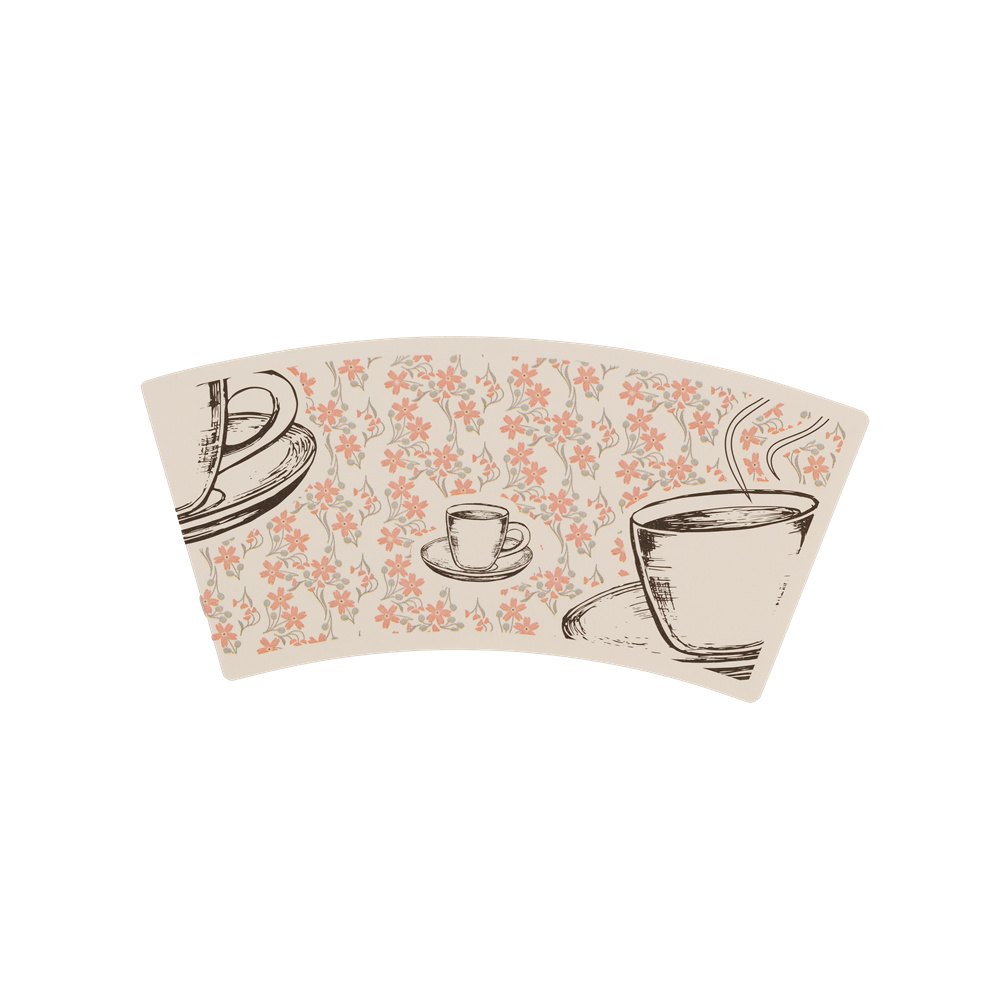
A paper cup raw material manufacturer serves as a critical supplier in the beverage packaging industry, providing essential materials that form the foundation of disposable cup production. These manufacturers specialize in sourcing and processing premium-grade paper substrates, coating compounds, and adhesive solutions specifically designed for cup manufacturing applications. The paper cup raw material manufacturer operates sophisticated production facilities equipped with advanced machinery that ensures consistent material quality and specifications. The primary function of a paper cup raw material manufacturer involves transforming raw cellulose fibers into refined paper stock suitable for hot and cold beverage applications. This specialized manufacturer applies proprietary coating technologies that create moisture barriers, grease resistance, and thermal protection properties. Technological features include precision calendering systems, multi-layer lamination capabilities, and rigorous quality control protocols ensuring compliance with food safety standards. Applications for materials from a paper cup raw material manufacturer extend across numerous sectors including fast-food chains, coffee shops, beverage distribution companies, and catering services. The manufacturer tailors product specifications to meet diverse requirements, from lightweight single-wall cups to reinforced multi-layer constructions. By partnering with a reliable paper cup raw material manufacturer, businesses gain access to consistent, high-performance materials that directly impact their end-product quality and brand reputation. These suppliers also offer customization options, technical support, and sustainable sourcing alternatives that enable customers to meet environmental objectives while maintaining operational efficiency.
Selecting a reputable paper cup raw material manufacturer delivers substantial operational and financial benefits to beverage packaging companies. Quality assurance represents a primary advantage, as established manufacturers implement comprehensive testing protocols ensuring every batch meets international food safety regulations and industry standards. This commitment reduces defect rates, minimizes waste, and protects customer satisfaction. Cost efficiency emerges as another significant benefit when working with a paper cup raw material manufacturer. Large-scale production capabilities and established supply chains allow these manufacturers to offer competitive pricing without compromising material integrity. Bulk purchasing options provide further savings, enabling businesses to optimize their production budgets while maintaining consistent material access. Operational reliability distinguishes a professional paper cup raw material manufacturer from competitors. Consistent material specifications ensure seamless integration into existing production equipment, reducing downtime and setup complications. Reliable delivery schedules and inventory management support prevent production interruptions and supply chain disruptions. The paper cup raw material manufacturer also provides customization flexibility, allowing businesses to select specific coating formulations, thickness variations, and sustainability features matching their unique requirements. Technical expertise and dedicated customer support teams assist in material selection and troubleshooting, enabling informed decision-making. Environmental responsibility has become increasingly important. Many paper cup raw material manufacturers now offer eco-friendly alternatives, including recycled content options and compostable coatings, helping businesses reduce their environmental footprint while meeting consumer expectations. Access to innovation represents another advantage, as manufacturers continuously develop improved formulations responding to market demands for better performance and sustainability. Finally, partnering with an established paper cup raw material manufacturer provides supply chain stability and long-term business security, allowing companies to focus on core operations while depending on reliable material provision.

Latest News

Industry News: Customized Eco-friendly Paper Cups Lead New Trends in Catering and Events

29

May

Industry News: Customized Eco-friendly Paper Cups Lead New Trends in Catering and Events

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Advanced Material Science and Quality Control

Advanced Material Science and Quality Control

A professional paper cup raw material manufacturer employs cutting-edge material science techniques to develop superior paper compositions. These manufacturers invest heavily in research and development, creating proprietary formulations that enhance cup performance and durability. The paper cup raw material manufacturer utilizes state-of-the-art quality control systems including automated testing equipment, spectroscopic analysis, and mechanical property assessments. Every production batch undergoes rigorous evaluation ensuring consistent fiber strength, coating adhesion, and barrier functionality. Advanced laboratory facilities enable manufacturers to test materials under extreme conditions, simulating real-world beverage storage scenarios. This commitment to quality assurance guarantees that end customers receive cups meeting exact specifications and performance standards, whether for hot beverages requiring thermal protection or cold drinks needing moisture resistance and structural integrity.
Sustainable Production and Eco-Conscious Solutions

Sustainable Production and Eco-Conscious Solutions

Modern paper cup raw material manufacturers prioritize environmental responsibility throughout their operations. These companies source sustainably harvested cellulose from responsibly managed forests and implement energy-efficient production processes minimizing carbon emissions. The paper cup raw material manufacturer develops eco-friendly coating alternatives using water-based formulations and compostable polymer solutions that reduce environmental impact. Many manufacturers achieve industry certifications demonstrating compliance with environmental standards and sustainable practices. By choosing a manufacturer committed to sustainability, businesses demonstrate environmental stewardship while meeting consumer expectations for responsible packaging. The paper cup raw material manufacturer also facilitates circular economy initiatives by developing recyclable paper stock and promoting material recovery programs, enabling customers to support environmental conservation objectives without sacrificing product performance or operational efficiency.
Technical Support and Customization Capabilities

Technical Support and Customization Capabilities

A leading paper cup raw material manufacturer provides comprehensive technical expertise and personalized customization services tailored to specific customer needs. These manufacturers employ experienced engineers and material scientists available for consultation, helping businesses select optimal material specifications for their particular applications. The paper cup raw material manufacturer offers extensive customization options including varied coating thicknesses, specialized barrier treatments, and color variants accommodating diverse branding requirements. Technical teams assist with equipment compatibility assessments, ensuring sourced materials integrate seamlessly with existing production systems. Manufacturers provide detailed technical documentation, performance data, and application guidance enabling informed purchasing decisions. Additionally, the paper cup raw material manufacturer maintains responsive customer support addressing concerns, troubleshooting issues, and adjusting formulations when market demands evolve, establishing long-term partnerships built on trust and collaborative problem-solving.