Coloured Paper Cups: Premium Beverage Solutions

, , 
Inquiry
Inquiry

coloured paper cups

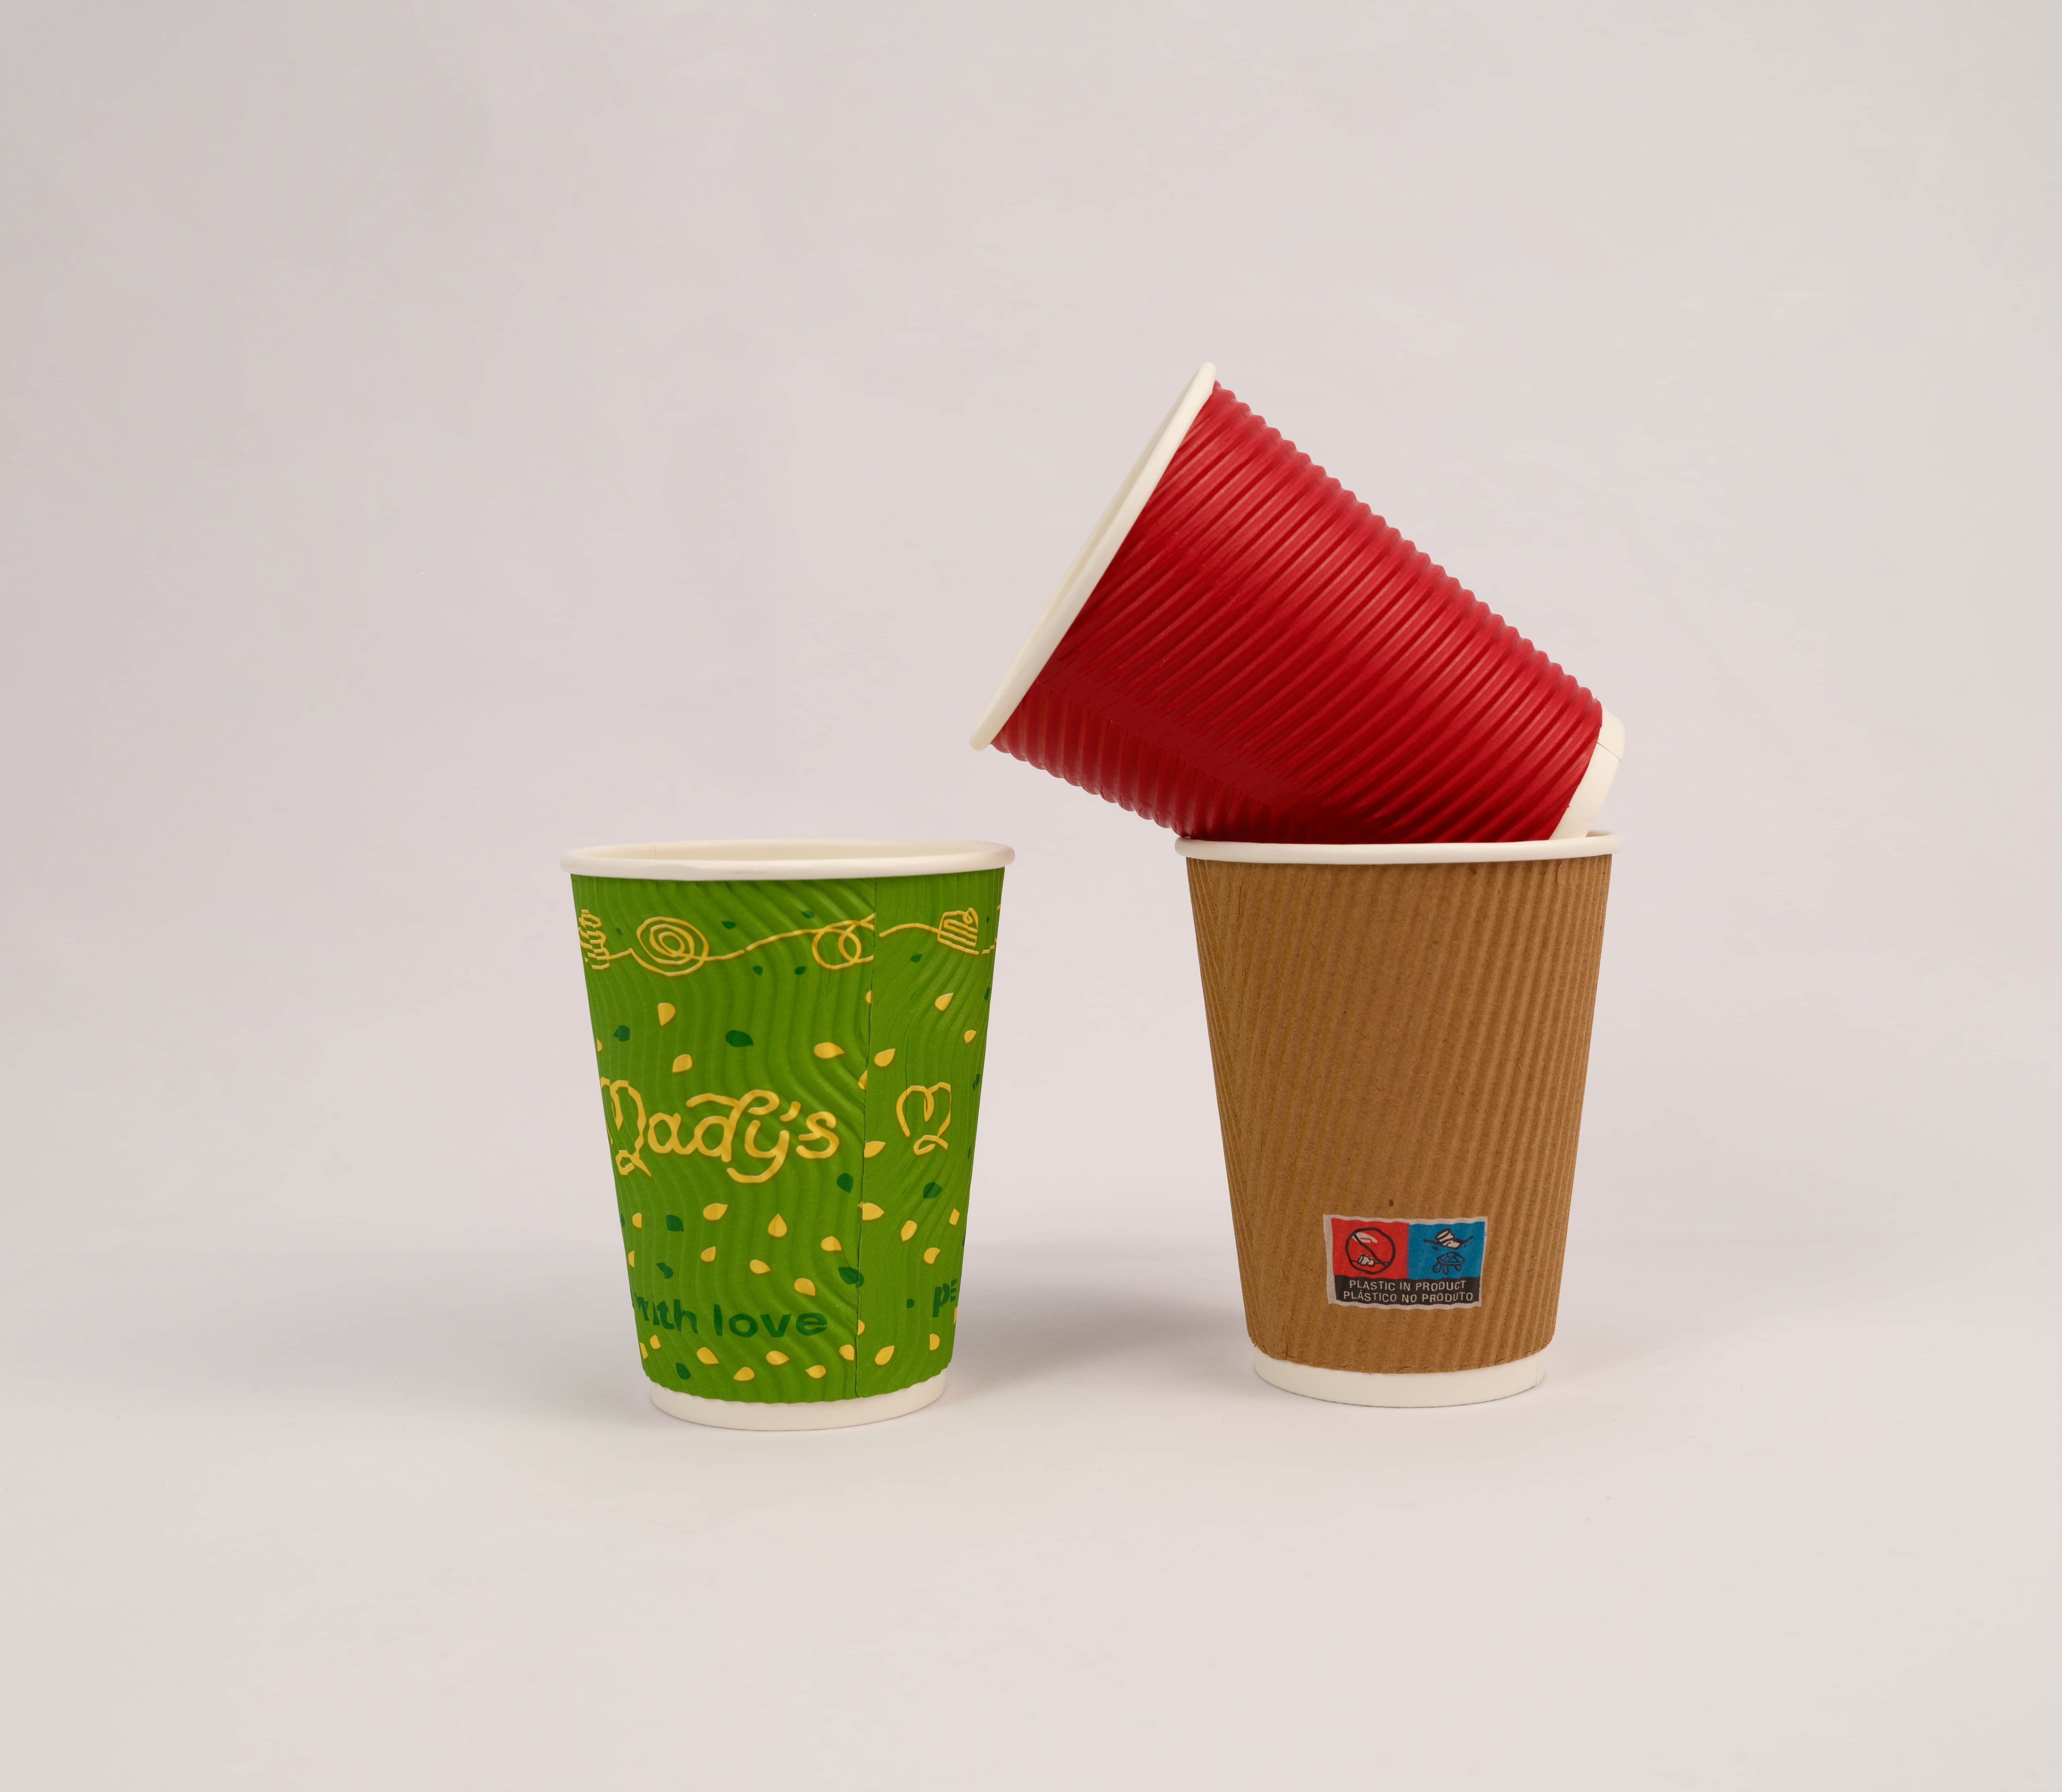
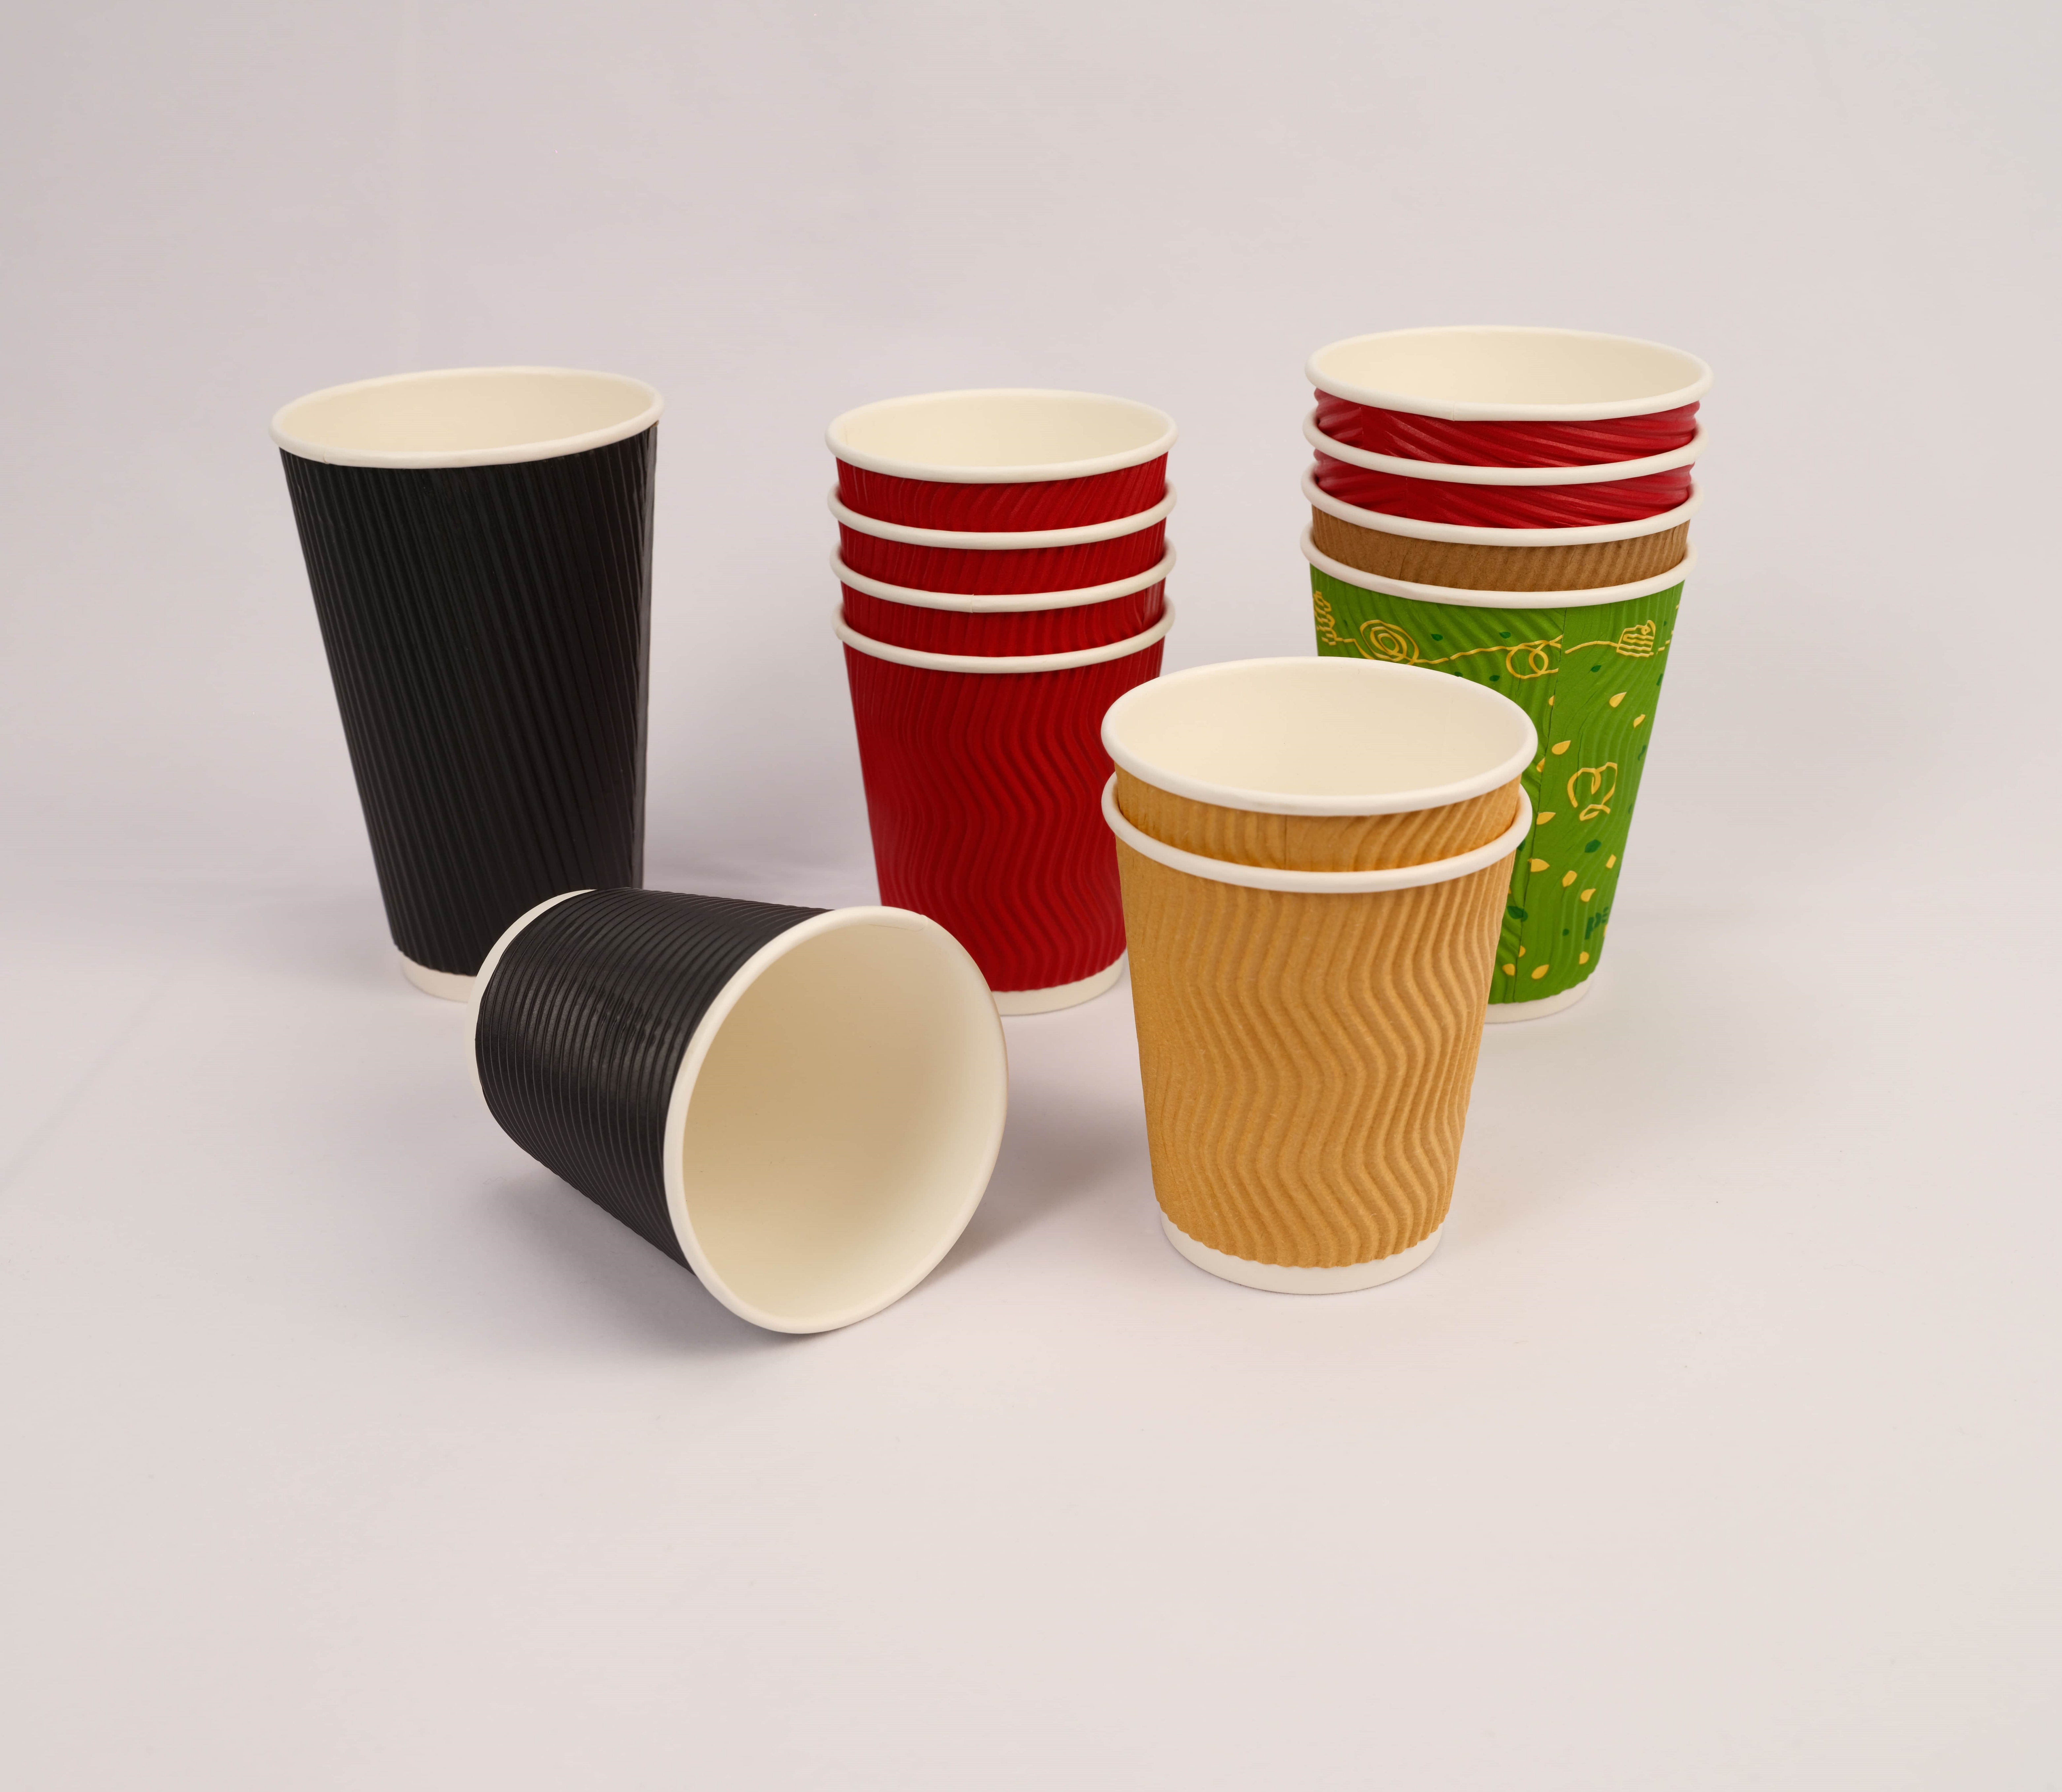
Coloured paper cups represent a versatile and practical solution for beverage service across multiple industries and settings. These innovative coloured paper cups combine functionality with aesthetic appeal, making them ideal for cafes, restaurants, events, and retail environments. Coloured paper cups are manufactured using high-quality paper materials that provide durability while maintaining environmental consciousness. The primary function of coloured paper cups is to safely contain hot and cold beverages while delivering an attractive presentation. These coloured paper cups feature advanced insulation technology that protects hands from temperature extremes and preserves drink quality. The technological features embedded in coloured paper cups include food-grade paper construction, water-resistant coatings, and structural reinforcement that prevents leakage and maintains integrity during transport. Coloured paper cups serve diverse applications ranging from coffee shops and smoothie bars to corporate events and outdoor gatherings. Their vibrant colour options enable brand customization and visual differentiation in competitive markets. The cups accommodate various sizes, typically ranging from 8 ounces to 20 ounces, adapting to different beverage types and serving preferences. Modern coloured paper cups incorporate eco-friendly materials that reduce environmental impact without compromising performance. These cups feature secure base construction and smooth rim finishing that enhances user experience. The versatility of coloured paper cups extends to customization possibilities, allowing businesses to incorporate logos, designs, and messaging that reinforce brand identity and customer engagement throughout the entire beverage service experience.
Coloured paper cups deliver exceptional value to businesses seeking reliable beverage service solutions with distinctive branding opportunities. These cups provide immediate practical benefits through superior heat insulation that prevents condensation and hand discomfort, ensuring customer satisfaction with every sip. The operational advantages of coloured paper cups include lightweight construction that reduces shipping costs and storage requirements compared to ceramic or glass alternatives. From an application perspective, coloured paper cups excel across diverse settings including quick-service restaurants, specialty coffee shops, catering services, and outdoor events. Their stackable design maximizes storage efficiency while maintaining product integrity, allowing businesses to maintain adequate inventory without excessive space consumption. The customization potential of coloured paper cups enables companies to strengthen brand recognition through distinctive colour schemes and printed messaging that create memorable customer interactions. Practical buyer value extends to cost-effectiveness, as coloured paper cups offer competitive pricing without sacrificing quality or performance standards. These cups eliminate labour-intensive washing and sanitation processes associated with reusable alternatives, streamlining operational workflows and reducing maintenance expenses. The decision-useful context shows coloured paper cups provide environmental advantages through recyclable materials and reduced water consumption during production and service delivery. Additionally, coloured paper cups accommodate dietary preferences and health-conscious consumers through certified food-grade composition that meets international safety standards. The barrier coatings prevent beverage absorption and maintain flavour integrity while protecting contents from external contamination. Businesses benefit from reduced liability exposure through disposable usage that eliminates cross-contamination risks. The versatility of coloured paper cups ensures suitability for hot coffee, iced beverages, and specialty drinks, making them indispensable for comprehensive beverage programs serving diverse customer preferences and operational requirements.

Practical Tips

Industry News: PE/PLA Coated Paper Leads New Environmental Trend in Food Packaging

29

May

Industry News: PE/PLA Coated Paper Leads New Environmental Trend in Food Packaging

View More
Industry News: Paper Cup Fan (Paper Cup Blank) Technical Innovation Drives New Upgrades in Beverage Packaging

29

May

Industry News: Paper Cup Fan (Paper Cup Blank) Technical Innovation Drives New Upgrades in Beverage Packaging

View More

Get a Free Quote

Our representative will contact you soon.
0/1000
Premium Insulation Technology for Temperature Protection

Premium Insulation Technology for Temperature Protection

Coloured paper cups incorporate advanced double-wall insulation technology that maintains optimal beverage temperatures while protecting consumer hands from extreme heat or cold. This technological innovation distinguishes coloured paper cups from basic single-wall alternatives, providing superior performance in demanding service environments. The insulation properties prevent condensation formation on cup exteriors, eliminating uncomfortable wet surfaces and protecting customer clothing from moisture damage. The thermal barrier within coloured paper cups ensures beverages remain at desired temperatures longer, enhancing overall consumption experience and customer satisfaction. This feature proves particularly valuable for coffee shops, tea services, and specialty beverage establishments where temperature maintenance directly impacts product quality perception. The advanced construction of coloured paper cups reduces heat transfer significantly, allowing customers to comfortably hold beverages immediately after service without requiring protective sleeves or excessive handling precautions. Businesses leveraging coloured paper cups with premium insulation technology gain competitive advantages through enhanced customer experiences and reduced complaints related to beverage temperature or hand comfort issues.
Sustainable Manufacturing and Eco-Friendly Material Composition

Sustainable Manufacturing and Eco-Friendly Material Composition

Coloured paper cups are manufactured using responsibly sourced paper materials that prioritize environmental sustainability without compromising functional performance or durability standards. These environmentally conscious coloured paper cups feature recyclable composition that supports circular economy principles and reduces landfill contributions. The manufacturing process for coloured paper cups minimizes water consumption and chemical waste compared to alternative beverage container technologies, aligning with corporate sustainability objectives and regulatory compliance requirements. The eco-friendly attributes of coloured paper cups appeal to environmentally conscious consumers and businesses committed to reducing carbon footprints. These cups utilize food-grade coatings derived from sustainable sources that eliminate harmful chemical exposure while maintaining product safety and integrity. Organisations selecting coloured paper cups demonstrate environmental commitment, enhancing brand reputation and customer loyalty among sustainability-focused demographics. The responsible production methods embedded in coloured paper cups reflect modern business values emphasizing ecological stewardship, renewable resource management, and waste reduction initiatives. This sustainable positioning of coloured paper cups creates competitive differentiation in markets increasingly valuing corporate environmental responsibility.
Customizable Branding and Vibrant Colour Options

Customizable Branding and Vibrant Colour Options

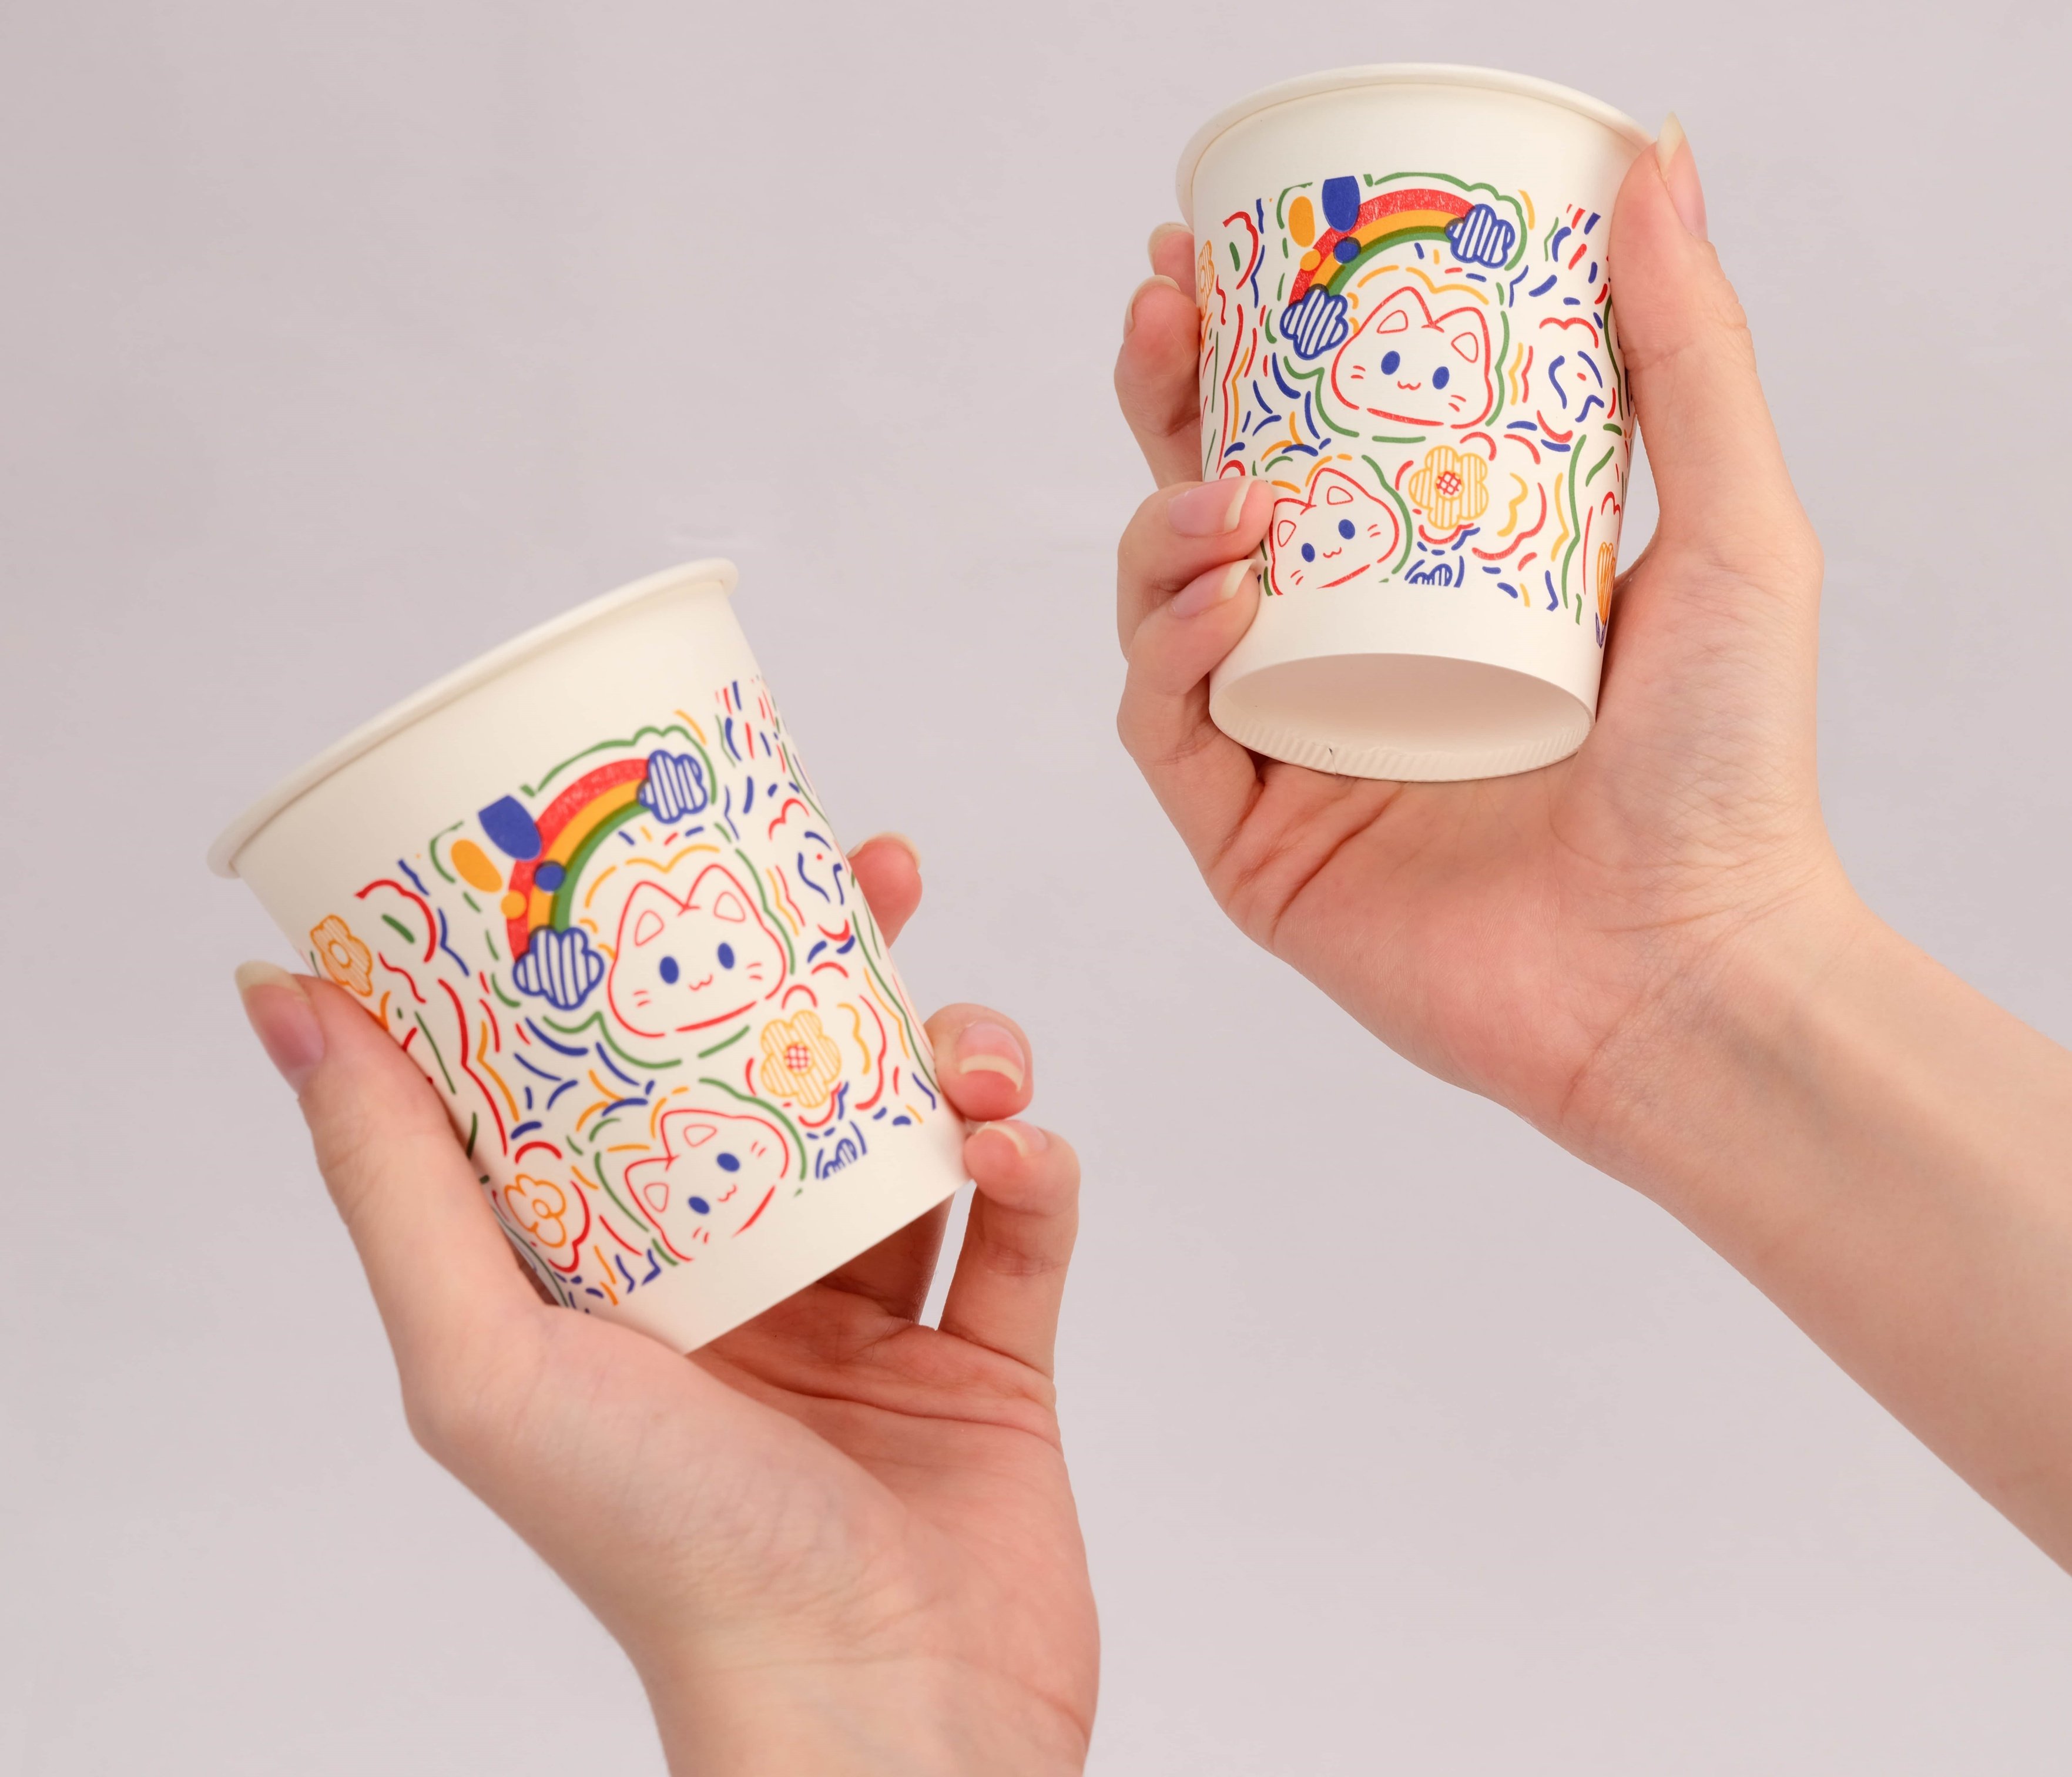
Coloured paper cups offer unlimited customization possibilities enabling businesses to showcase distinctive branding through vibrant colour selections and personalized design implementations. These versatile coloured paper cups accommodate custom printing of logos, messaging, promotional content, and artistic designs that transform ordinary beverage containers into powerful marketing vehicles. The high-quality printing capabilities on coloured paper cups ensure brand imagery remains vivid and professional throughout the entire customer experience, creating lasting visual impressions. The colour variety available in coloured paper cups enables businesses to align beverage packaging with brand identity, seasonal campaigns, or special promotional initiatives. Custom coloured paper cups serve as mobile advertisements, carrying brand messages throughout communities as customers transport beverages during daily activities. The psychological impact of colour selection in coloured paper cups influences consumer perception and purchase decisions, making customization strategically important for competitive differentiation. Organisations utilising coloured paper cups with personalized branding experience enhanced customer recognition, improved brand recall, and strengthened emotional connections with target audiences. This branding flexibility distinguishes coloured paper cups as essential tools for modern marketing strategies seeking tangible, functional brand engagement opportunities.